
Satisfies 1 requirement
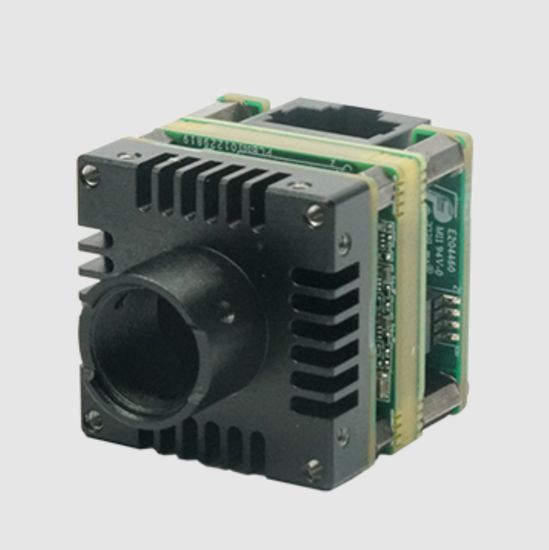
Industrial Machine Vision Camera High Frame Rate Gige 640*480 1/4" Mono CMOS Global Shutter Camera for Machine Intelligent Positioning Detection
US$169.90-699.90
1 Piece(MOQ)
I have found results from60000+products and20000+suppliers aboutMachine vision camera




Selecting the correct sensor depends on your inspection accuracy requirements. For high-speed production lines, Global Shutter sensors are essential to avoid motion blur, whereas Rolling Shutter sensors are more cost-effective for static objects. Resolution should be calculated based on your Field of View (FOV) and the minimum feature size you need to detect; typically, a feature should be covered by at least 3 to 5 pixels for reliable analysis.
The choice of interface affects bandwidth and cable length. GigE Vision is the most popular for long-distance transmission (up to 100m) and easy integration into existing networks. For high-speed data transfer, USB 3.0 (USB3 Vision) offers plug-and-play convenience for shorter distances, while Camera Link or CoaXPress are reserved for ultra-high-bandwidth applications requiring zero-latency and massive data throughput.
To ensure safety and interoperability, verify that the cameras carry CE (Europe) and FCC (USA) certifications. For industrial environments, RoHS compliance is necessary to meet environmental regulations. Furthermore, ensure the hardware supports the GenICam (Generic Interface for Cameras) standard, which guarantees that the software can recognize and control the camera regardless of the physical interface.
Industrial cameras often operate in harsh conditions. Check the IP Rating (Ingress Protection); an IP67 rating is vital if the camera is exposed to dust or water splashes. Additionally, confirm the operating temperature range (typically 0°C to 50°C) and look for shock and vibration resistance specifications (e.g., IEC 60068-2-27) to ensure long-term stability on robotic arms or vibrating machinery.
The main risks include optical misalignment during transit and firmware incompatibility. Always insist on protective anti-static packaging and vacuum-sealed bags. Before shipping, request a factory calibration report and a video demonstration of the specific units being tested with the latest firmware version to avoid costly returns.
Focus on Total Cost of Ownership (TCO) rather than just the unit price. Negotiate for extended warranties (2-3 years) and SDK (Software Development Kit) support. For volume orders, ask for tiered pricing where the discount increases as your annual procurement volume grows, and try to secure free technical integration consulting as part of the package.
Utilize secure payment methods and consider third-party pre-shipment inspections to verify pixel defects (dead pixels) and sensor cleanliness. When sourcing via Made-in-China.com, prioritize Audited Suppliers who have undergone on-site verification of their manufacturing capabilities and quality management systems.
Machine vision cameras are sensitive electronics; use reputable express couriers (DHL/FedEx/UPS) for better handling and tracking. Ensure the HS Code (typically 8525.80) is correctly declared to avoid customs delays. For large batches to specific regions, clarify Incoterms (FOB or DAP) to define exactly who bears the risk and cost of import duties and local clearance.